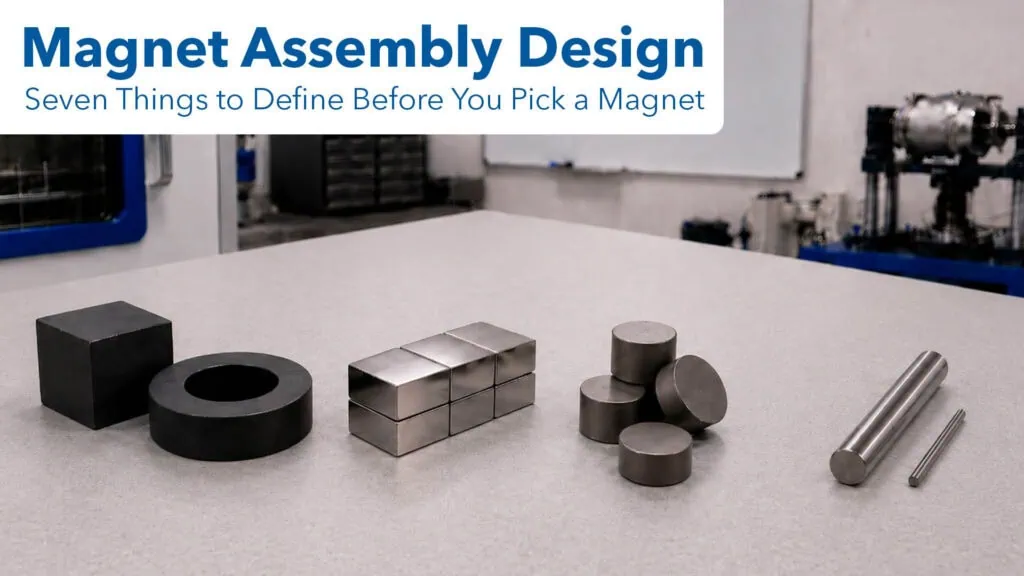
Magnetic Assembly Design: Seven Things to Define Before You Pick a Magnet
An engineer sends us a drawing with a magnet called out by grade and dimension, and asks whether we can build the assembly. About half the time the answer involves going backwards first, because the grade was chosen before anyone checked what temperature the part runs at, or how much steel sits behind the magnet in the final product.
That is not a criticism of the engineer. Magnetic assembly design sits at an awkward intersection of magnetics, mechanical design and manufacturing, and most mechanical engineers do one of those three every day and the other two occasionally. The seven inputs below are what our applications engineers ask for. Having answers to them, even rough ones, is what makes a first conversation productive.
1. What the field has to do, and where
Start with a functional requirement rather than a magnetic one. “Hold a 3 pound cover closed against vibration” and “switch a Hall sensor at 5 millimeters” are both useful. “We need a strong magnet” is not, because strength alone does not tell us the geometry, and geometry is where most of the performance lives.
The two specifics that matter most are the working distance and the working face. A magnet that delivers plenty of field at contact may deliver very little at 5 millimeters, because field falls off quickly with distance. If the requirement involves a gap, define the gap early. It changes the material decision and it often changes the construction entirely.
2. The operating temperature the magnet actually sees
Not ambient. Not the room the machine sits in. The highest temperature the magnet experiences in service, including heat the rest of the product puts into it.
Temperature drives magnetic assembly design harder than any other environmental factor. Every permanent magnet loses output as it heats, and part of that loss is reversible while part of it is not. A magnet taken above its maximum operating temperature comes back permanently weaker, and no amount of cooling recovers it. Because maximum operating temperature depends on the magnet’s geometry and the surrounding magnetic circuit, not just its grade, the published figures for a material family are a starting point rather than an answer.
If you know the temperature, we can select against it. If the temperature is genuinely unknown, say so, because designing with margin for an unknown is a different exercise than designing to a number.
3. What the magnetic circuit looks like
A bare magnet radiates field in all directions and wastes most of it. Put a steel cup around it, or a plate behind it, and that flux gets redirected toward the working face. This is why an assembly frequently outperforms a larger loose magnet, and why buying a stronger magnet is often the more expensive way to solve a field problem.
The circuit does not stop at your part. Whatever your assembly mounts to becomes part of the circuit too. Steel structure near the assembly will pull field, and a design validated on a bench with nothing around it can behave differently once installed. Tell us what the assembly mounts to.
4. How the magnet stays where you put it
Retention is where a surprising share of field failures originate. The bond, press fit, staking or fastener holding the magnet has to survive the same temperature, chemistry, shock and vibration as the magnet itself, and adhesives in particular have temperature limits that are frequently lower than the magnet’s.
Decide early whether the retention method is bonded, mechanical, or both. That decision constrains the housing design and sometimes the magnet geometry, which is why it is cheaper to make at concept stage.
5. What has to be held to a tolerance, and what does not
Every magnetic assembly has a few dimensions that matter and many that do not. Positional tolerance on the magnet relative to the working face usually matters. Cosmetic dimensions on the housing usually do not. Calling out tight tolerances everywhere raises cost without improving function, and calling out none leaves the important ones to chance.
The tolerances achievable on a given feature depend on material, geometry and process, so we will confirm what is realistic for your specific part rather than quoting a general figure.
6. Quantity, now and later
Prototype quantity and production quantity lead to different constructions. A design that is straightforward to build five of by hand may need fixturing, different retention, or a different magnet geometry to build two thousand of consistently. Knowing the eventual volume during design avoids redesigning the part at exactly the moment the program can least afford it.
7. How you will know a finished assembly is good
Agree the verification method before the first article, not after. Field measurement at a defined point, a functional check against the requirement, or a dimensional inspection all answer different questions. The acceptance criterion should trace back to item 1 on this list, which is why it is worth writing the functional requirement down properly.
Bring the requirement, not just the part
Adams Magnetic Products has built custom magnetic assemblies for instrumentation, actuator, industrial and medical applications since 1950, and the projects that go smoothly are consistently the ones where these seven items were discussed before the drawing was finished.
You do not need answers to all seven to start. Bring what you have. If you have a drawing, Send Us Your Drawing for an engineering review. If you are earlier than that, Talk to a Magnet Expert with your field requirement, operating temperature and available space, and we will help define the rest.
Related Posts